Ir a contenido
Not Sure Which Welder Fits Your Application? Start With a Free Micro-Weld Evaluation

Drone & UAV Manufacturing

Micro Welding for UAV and Drone Manufacturing

Battery packs, motor windings, airframes, sensor housings, harnesses, and boards

UAV joints often sit beside heat-sensitive cells, windings, electronics, and precision components. A sound weld must form without transferring excess heat into the surrounding assembly.

Sunstone micro welding systems span capacitive discharge, pulse arc, AC and DC resistance, fiber laser, and Nd:YAG laser technologies. We help you match energy delivery to the material, joint geometry, and production requirements.

Interactive Application Guide

Explore UAV Manufacturing Applications

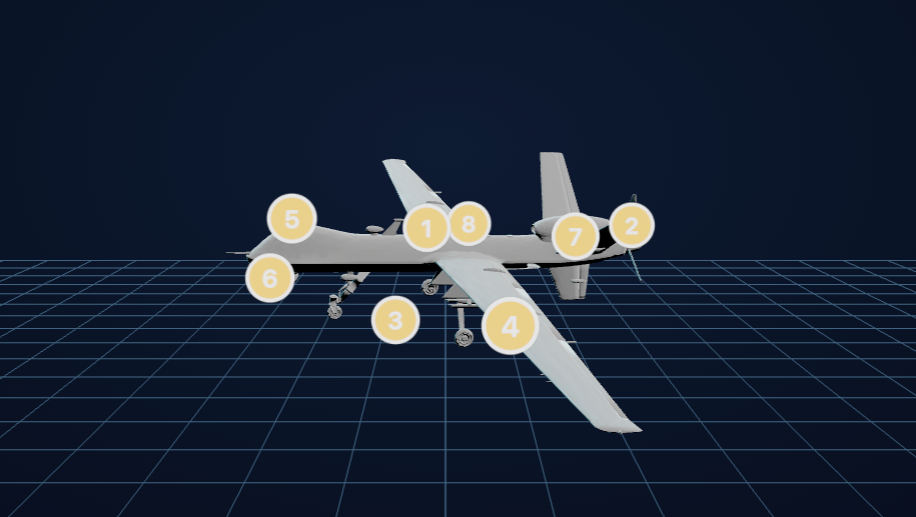
Select a numbered application on the UAV model to explore relevant welding, assembly, and part-marking solutions.

Explore UAV Manufacturing Applications

Airframe shown is stylized and illustrative. Applications apply across electric and combustion UAV platforms.

Have a joint you are not sure how to weld?

Send your parts to our fully staffed welding lab. We will evaluate the joint and return your samples with a detailed analysis that may include photos and video. There is no cost and no obligation.

Find the right process for your joint

Compare common UAV manufacturing components with potential welding processes and Sunstone system paths.

Component Material Thickness Process System
Battery tab to cell canNickel, aluminum, SigmaClad®Up to 0.010" (0.25 mm)Capacitive dischargeCDDP-A series
Copper battery tabPure copper0.003" to 0.025" (0.08 to 0.64 mm)Pulse arcOmega PA250i
Battery tabs, busbars, cell housingsCopper, nickel, aluminum, SigmaClad®Up to 0.040" (1.0 mm)Fiber laserSFL 1500 / SFL 3000
Magnet wire to terminal, coating intactEnameled copperFineThermocompressionPico DC with Micro E
Magnet wire to terminal, coating removedBare copperFineLaser, pulse arc, or resistanceLZR, Orion, or CDDP-A
Stranded phase lead to terminalStranded copper, brassVaries by gaugeResistance or pulse arcCDDP-A or Orion
Harness conductor to terminalTinned and bare copper, brassVaries by gaugeHF inverter resistanceAeon HF
Airframe tubes, motor mounts, bracketsTitanium, aluminum, stainless, InconelThin wallPulsed Nd:YAG or fiber laserOrion LZR 300 Pro Max or SFL
Flex circuit to boardCopper, solder, padsFine pitchHot bar reflowHot Bar Pulse Heat
Wire to padFine copper wire1 to 3 milThermocompressionPico DC with Micro E
Sensor enclosure hermetic seamStainless, titanium, KovarThin wallAC resistance, seam modeWave AC
Coax braid to groundCopper braidFine braidDC resistancePico DC
SMA and MMCX connectorsPlated brassFine pitchHot bar reflowHot Bar Pulse Heat
Part markingTitanium, aluminum, stainless, plasticsSurfaceFiber laser markingOrion Pro Series Engraver

Thickness capability depends on material, weld geometry, and application. Contact us to validate your specific parts.

Welding by UAV application

Explore the process considerations behind each joint, from battery tabs and motor leads to structural welds and part identification.

Battery and power systems

Nickel, aluminum, and SigmaClad® tabs

Heat control is central to battery welding. Excess heat conducted through the cell housing can damage the internal separator, so the process must concentrate energy at the tab-to-can interface. The CDDP-A stores energy in capacitors and releases it in a controlled burst for a localized heat-affected zone. Stored energy also reduces sensitivity to line-voltage fluctuations.

Four models span 200 to 1,200 watt-seconds of stored energy. Tab thickness, cell format, and can material determine the appropriate model. Additional capacity can accommodate future pack designs; validate the selection on your own parts.

Copper tabs

Copper carries heat away from the joint quickly, making it challenging for some resistance processes. The Omega PA250i delivers a metered pulse arc through a tungsten electrode. The application range is 0.003 to 0.025 inches for pure copper and up to 0.020 inches for SigmaClad®; capability depends on the joint.

Stylus, weld-head, and CNC configurations support work from development to automated production. PLC integration is available for production lines.

Production volume

The SFL Series is an integrated fiber laser cell for 18650 and 21700 cylindrical modules, prismatic assemblies, busbar-to-terminal connections, and cell housing seams. The 1,500 W and 3,000 W configurations combine X–Y motion with two-axis galvo scanning over a 1000 × 800 mm working area.

Review facility requirements early: 480 V three-phase power, 15–20 kVA for the 1,500 W configuration or 30–40 kVA for the 3,000 W configuration, deionized-water cooling with a 16-liter minimum, shielding gas, and compressed air. The enclosed cell and final configuration should be reviewed with the applications team. SFL pricing is configuration-specific.

Brushless motors and ESCs

Settle the coating requirement first

Magnet wire is copper with a thin enamel coating. With the coating intact, thermocompression applies heat and force together to displace the coating at the contact point. The Pico DC paired with the Micro E weld head supports this work.

Removing the coating opens up laser, pulse arc, and resistance welding options. Wire gauge, terminal geometry, and proximity to the winding guide the choice. Stranded phase leads can use capacitive discharge resistance or pulse arc welding, subject to sample evaluation.

Pico DC with Micro E

The Pico DC offers closed-loop DC resistance control over 0.10–5.00 V, 10–250 A, and 1.0–650 W, with single- or dual-pulse weld times from 1–500 milliseconds. The Micro E provides 30–2,000 grams of force, one-micron positional accuracy, and 25 mm of travel.

Force and displacement monitoring requires both the Pico DC and Micro E. Include the welder, weld head, electrodes, and application tooling in the configuration review.

Wire harnesses and connectors

Aeon HF for repetitive terminations

A harness can contain hundreds of terminations exposed to sustained vibration. Welding can join the metals directly without added solder or flux. Joint geometry, conductor gauge, and production testing determine whether the process suits the assembly.

The Aeon HF provides up to 2,500 A at a 12% duty cycle, with a 40-microsecond feedback response. It monitors current, voltage, power, resistance, and displacement independently on each pulse. Protected schedules and Ethernet Modbus support remote schedule selection and weld-data collection.

Confirm facility power before specifying the system. Aeon HF configurations use 208, 400, or 480 VAC three-phase power.

Orion pulse arc for connector work

The Orion 150s offers 1–150 joules, a 0.5–3.5 mm weld spot, and up to nine welds per second for repetitive terminations. The Orion 200x offers 0.15–200 joules, a 0.1–4.5 mm spot, and classic, triangle, and square waveforms. Evaluate the process on your connector and conductor stack.

Frame and structure

Control distortion and shielding

Structural joints must meet both strength and dimensional requirements. Excess heat can warp a thin-wall tube or motor mount even when the weld itself is sound. Review applicable customer and program requirements during process development.

Titanium requires effective shielding during welding and cooling. Confirm gas coverage and pre-flow and post-flow timing for the selected system and joint.

Systems for structural work

The Orion LZR 300 Pro Max delivers up to 300 joules, 150 W average power, and 15 kW peak power, with a 0.1–2.0 mm spot and speeds up to 50 welds per second. Focused energy helps limit the heat-affected zone on thin-wall parts.

The SFL Series is another option for structural production, with welding, surface-cleaning, and cutting capabilities to evaluate against the application. For repair and rework, the Orion 200x combines controlled pulse arc energy with 5× optics.

PCBs and flight controllers

Hot bar pulse heat reflow

Hot bar reflow is selective soldering, not welding. A shaped thermode heats the joint pattern, melts the solder, and holds pressure until it solidifies. Digital PID temperature control supports repeatable profiles while monitoring upper and lower limits and detecting profile errors.

The system stores 15 settings and includes RS-232C and I/O for automation. It is compatible with lead-free solder. Hot bar systems are quoted by application and are available for sale in the United States only.

Parallel-gap welding

The Pico DC supports parallel-gap welding, with both electrodes on the same side of the joint. For wire-to-pad bonding at 1–3 mil wire diameters, evaluate a dual-pulse welder paired with a micro weld head. Validate the process against the pad, conductor, and board construction.

Sensors and payloads

Enclosure seams and internal leads

The Wave AC supports hermetic seams on enclosures and lids using continuous AC energy in seam mode. Weld-time adjustments to one hundredth of a second help control heat on thin-wall housings.

Package materials include stainless steel, titanium, and Kovar. Kovar’s thermal expansion closely matches borosilicate glass, making it useful around glass-to-metal seals. Fine internal leads can be evaluated with the Pico DC and Micro E for controlled energy and force.

Leak-testing requirements vary by application and industry. Send your parts and specification so the applications team can evaluate the joint against your requirements.

Antennas and RF

Match the process to the termination

Connection consistency affects RF performance. Where the braid is fine enough, the Pico DC provides controlled, low-energy resistance welding. Evaluate the actual cable and braid thickness before choosing the process.

For SMA and MMCX terminations that require soldering, hot bar pulse heat reflow delivers controlled heat and pressure within a small footprint. Hot bar systems are available for sale in the United States only.

Part marking and traceability

Permanent identification

Laser marking creates identifiers directly on compatible substrates without applying a label. It supports traceability for frames, ESC housings, boards, and other UAV components in titanium, aluminum, stainless steel, and suitable plastics.

Evaluate the marking process against the substrate, available marking area, and service environment. Browse laser engravers for part-identification options.

Drone & UAV Battery Production

Battery Pack Manufacturing Systems

Select a battery welding system around the tab material, cell format, joint geometry, and required throughput. Capacitive discharge, pulse arc, and fiber laser processes provide different ways to concentrate energy at the joint while limiting heat transfer into the cell.

Battery Tab Welding

CDDP-A Advanced Dual Pulse Spot Welder

Capacitive discharge welding for nickel, aluminum, and SigmaClad® battery tabs. Four models span 200–1,200 watt-seconds of stored energy. Select the weld head, electrodes, and tooling around your cell and tab design.
View the CDDP-A
Automated Battery Welding Configuration Required

Omega PA250i CNC Battery Welding System

An automated Omega configuration combining the PA250i, motorized weld-head control, and CNC motion for repeatable battery production. Final automation, fixturing, and process requirements are configured for the application.
Configure a CNC System
Fiber Laser Welding Configuration Required

SFL Fiber Laser Battery Welding Cell

A configured 1,500 W or 3,000 W fiber laser cell for cylindrical and prismatic modules, busbars, and cell housing seams. Review fixturing, throughput, cooling, gas, and three-phase power requirements with Sunstone.
Configure an SFL Cell

Precision Electronics Assembly

Electronics and Fine-Wire Welding Systems

Match precision resistance welding to fine motor wires, sensor leads, and wire-to-pad joints. Magnet wire with intact enamel calls for thermocompression; stripped wire opens up additional process options. Specify the power supply, weld head, electrodes, and tooling together.

Structural Components & Housings

Precision Laser Welding Systems

Control heat distortion in thin-wall tubes, brackets, mounts, and housings. Pulsed Nd:YAG and fiber laser systems concentrate energy at the joint. Select power, shielding, fixturing, and automation against your dimensional and production requirements.

Prototyping, Repair & Rework

General-Purpose Pulse Arc Welding Systems

Evaluate pulse arc welding for connector pins, stranded leads, prototype assembly, and localized repair. Match energy and weld controls to the material, conductor gauge, and terminal geometry, then validate the process on your parts.

Quality control and weld development

Develop the weld schedule

A weld schedule defines the parameters for your material stack and joint geometry. Destructive testing helps establish that schedule. Pull testing measures both failure force and failure mode; a tab that tears while its weld nuggets remain intact can indicate that the joint is stronger than the surrounding material.

Monitor the production process

Once the schedule is established, monitoring helps detect welds outside the defined process limits. The Pico DC with Micro E monitors force and displacement. The Aeon HF monitors current, voltage, power, resistance, and displacement on each pulse. CDDP-A weld monitoring and statistical process control tools help identify process drift over time.

Use process monitoring alongside the inspection and test plan required for your application. Monitoring supports production consistency; it does not by itself establish joint strength or replace required qualification tests.

Keep records and protect settings

CDDP-A, Pico DC, and Aeon HF platforms support weld-data export. Review timestamp feedback, setting lockout, remote schedule selection, and configuration cloning for your selected system and production workflow.

Working with Sunstone

Sunstone systems are designed, engineered, and manufactured in the United States, with U.S.-based engineering, service, and support. Learn about ISO 9001 certification and GSA compliance, or explore related aerospace and defense applications.

Warranty coverage is two years on the Omega PA250i, Aeon HF, and Micro E weld head, and three years on Orion x-Series and LZR systems. Review coverage for your selected configuration when requesting pricing.

Most systems have published product-page pricing. SFL cells are priced by configuration, and specialty systems are quoted by application. Hot bar reflow and seam sealing systems are available for sale in the United States only; other systems ship worldwide.

Prove it on your parts

For more than twenty years, Sunstone has helped manufacturers evaluate applications in our welding lab. Send your components so we can identify a suitable process and return your samples with a detailed analysis that may include photos and video. There is no cost and no obligation.

Still defining the application? Call or text our team for help deciding what to send.